AI Governance Checklist for Automation Projects in Regulated Industries
October 12, 2026 - AI

October 09, 2026 - AI
A cobot and a traditional industrial robot can both pick a part off a conveyor and set it into a fixture. The resemblance mostly ends there. One is built to work beside people, often with no fence at all. The other is built to move fast and carry real weight, and it does that best when humans stay outside a guarded cell. For a small factory planning its first automation project, the choice is rarely about which machine is better. It is about which set of trade-offs you can live with for the next five to ten years.
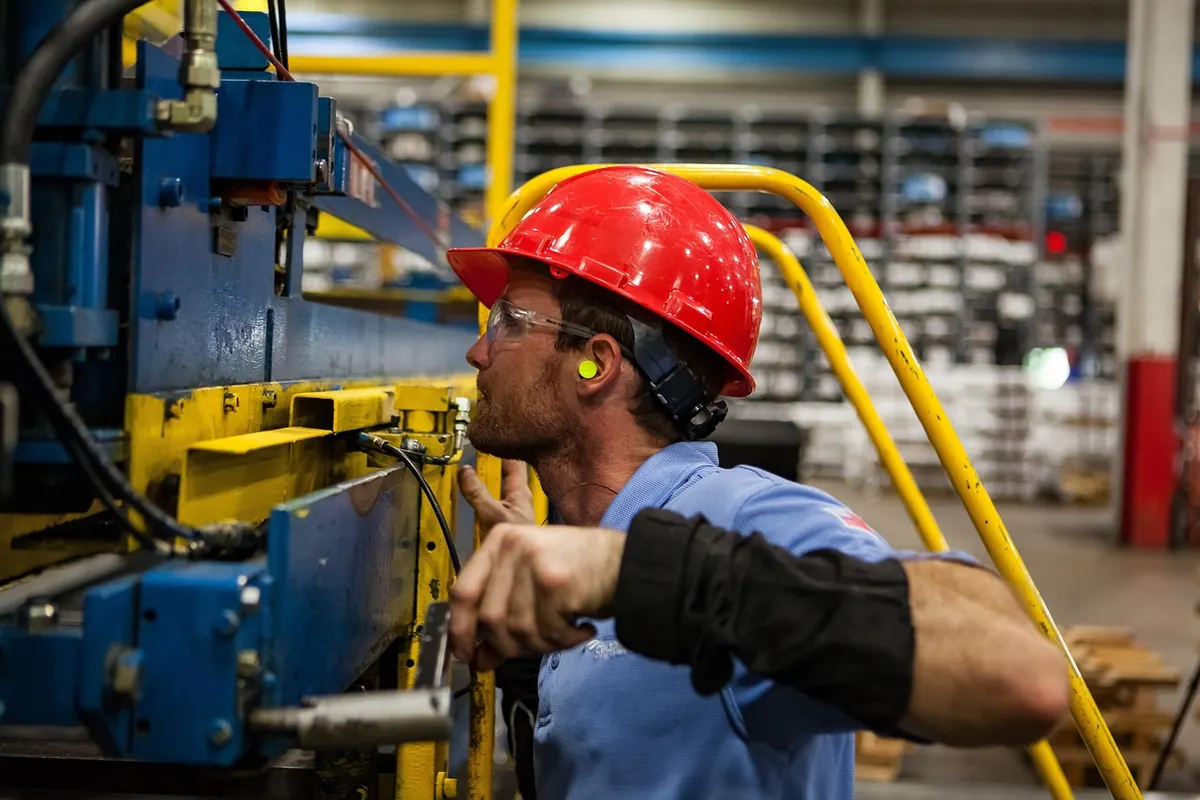
Traditional industrial robots come out of high-volume production. They are stiff, fast, and precise, and they usually sit inside a cage with light curtains and interlocks to keep people away from the moving arm. Payload and reach scale up well, and many run for years with modest maintenance.
Cobots were designed around a different assumption: that a person may be standing right next to the arm. Rounded joints, joint torque sensing, and force-limiting control let a cobot stop or back off when it meets something unexpected. Most models top out somewhere between roughly 3 kg and 20 kg of payload, and they generally move slower than their caged cousins.
Both families fall under ISO 10218, with collaborative operation covered further in ISO/TS 15066. Those standards matter, but they do not certify a cell as safe by themselves. Someone still has to look at your actual task.
A traditional six-axis arm often costs less per kilogram of payload than a cobot. That comparison collapses once you price the whole installation. A caged cell adds fencing, safety relays, guarding around the tooling, and integration hours. Floor space is a cost too, especially if you rent a tight unit and the cell eats an area you could use for a bench or a second machine.
A cobot usually needs far less guarding. It often bolts to an existing table, runs on a standard supply, and gets programmed the same afternoon. That does not make it cheap. You still pay for an end effector, a stand or fixture, cabling, and the risk assessment that has to happen either way.
There is also a throughput trap. If a cobot needs three times as long per cycle, buying two of them to match one traditional robot changes the arithmetic fast. Compare installed cost per finished part, not per machine.
The common misunderstanding is that a cobot is safe by definition. It is not. Hand-guiding and force limiting reduce the chance of a crushing injury from the arm itself, which is why fencing can often be pared back or left out. The arm is only one part of the cell, though.
Watch for pinch points between the arm and the fixture, a gripper that closes with real force, sharp or hot workpieces, and parts a tool might drop. Power and force limits apply to the robot's body, not to the blade in its gripper or the heavy casting it is carrying. A slow cobot holding a sharp part can still cause a serious injury.
Traditional robots handle safety differently: keep people out, interlock the door, and make sure nobody defeats the guard to save a few seconds. That last part is a human problem, not an engineering one, and it is worth designing access points so operators have no reason to bypass them.
Neither approach removes the need for a documented risk assessment of the specific task. If nobody in-house has that experience, pay a qualified safety professional for a few hours before you buy anything.
Payload figures deserve suspicion. A cobot rated at 10 kg has to carry the gripper too, so a 2 kg gripper leaves roughly 8 kg for the part — less if the part is held far from the wrist, where torque builds. Keeping tooling and part weight comfortably below the rated maximum, often nearer half to two-thirds depending on reach, is ordinary practice rather than a rule of law.
Reach matters just as much. A long, thin part held at full extension is a different job from a compact one held close in. Speed is where cobots give most ground: if the task needs a cycle every few seconds, all day, a caged robot is usually the honest answer.
Traditional robots also tolerate environments cobots do not. Welding spatter, grinding dust, washdown, and radiant heat all call for a check of ingress ratings before you assume a cobot can go where your process lives.
Cobot installs are often described as a weekend project, and they can be. Bolt it down, plug it in, guide the arm through waypoints by hand, save the program, run it slowly, then speed it up. A simple pick-and-place can be running in a day or two.
Traditional cells are a project in the other sense. Site preparation, anchoring, guarding fabrication, safety wiring, and integrator commissioning usually run into weeks or months, and production often stops while it happens.
The cobot advantage shrinks when the task touches other equipment. Getting an arm to hand a part to a conveyor, a press, or a vision system takes real engineering, and that work looks similar on both sides of the fence.
Pick the single job that annoys your team most — the one somebody does for four hours a day with their shoulders at a bad angle. Time it, photograph it, measure the part weight, and note how often it changes. Then ask two integrators to quote the same task, one with a cobot and one with a caged robot, and insist both quotes include guarding, tooling, commissioning, and training.
If you can, run a paid trial on your own parts before signing. Vendors quote cycle times on ideal parts under ideal conditions. Your parts have burrs, your fixture flexes, and your operators will find the edge cases within the first week.
Whatever you choose, budget for the person who will own the machine. A robot with no internal owner becomes a very expensive coat rack, and that is the one cost no comparison table ever captures.
Photo: geralt / Pixabay
A practical governance checklist for automation projects in regulated industries: bias audits, replayable audit...
A practical walkthrough of building an invoice pipeline that captures, extracts, validates and routes documents...
Copyright © 2026 Automation Alley. All Right Reserved.